01
Belt Conveyors
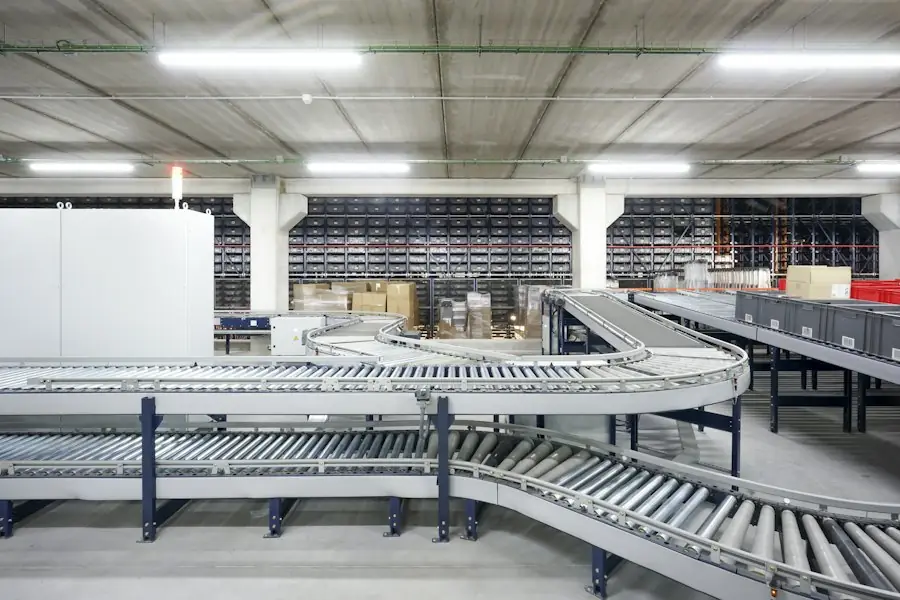
We supply belt conveyors and the components that wear out on them: conveyor belts, idlers, pulleys, belt cleaners, bucket elevators, screw conveyors, feeders and crusher spares. Supply covers new conveying lines, extensions to existing systems and replacement parts for plants already in operation.
Conveyor belt choice depends on what the belt carries. Fabric and steel-cord belts are specified for tension and length, heat-resistant grades for hot clinker, sinter and scale, and oil- and chemical-resistant grades for fertilizer and process materials. Share the material, temperature, belt width and conveyor length, and the belt is specified to suit the duty rather than the lowest price.
Idlers and pulleys are supplied to your existing frame dimensions and belt width, with lagging selected for the drive conditions. For bucket elevators we supply buckets, chains, belts and sprockets for cement, fertilizer and power plant duties, matched to the existing elevator so they fit without modification.
Unplanned conveyor stoppages hold up the whole plant. Planning critical spares in advance, such as a spare belt length, drive pulleys and a stock of idlers, shortens downtime when a failure happens. We can help you prepare a spares list for your conveying system and supply it in one shipment.
Yes. Belts, idlers and pulleys to your conveyor width and duty.
Yes. Buckets, chains, belts and sprockets for cement, fertilizer and power plants.
Yes. Heat-resistant belts are supplied in grades selected for the material temperature on your conveyor.
Both. Complete conveyor systems as well as belts, idlers, pulleys and drive components for existing conveyors.
Belt width, length, type and rating of the existing belt, the material carried and its temperature, and the conveyor layout if available.